• An In-Depth Analysis of How Grinding Wheels Affect Cutting Tools
    Sep 30, 2026 An In-Depth Analysis of How Grinding Wheels Affect Cutting Tools
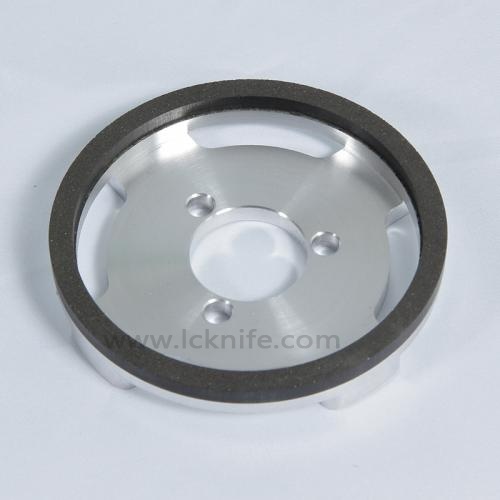
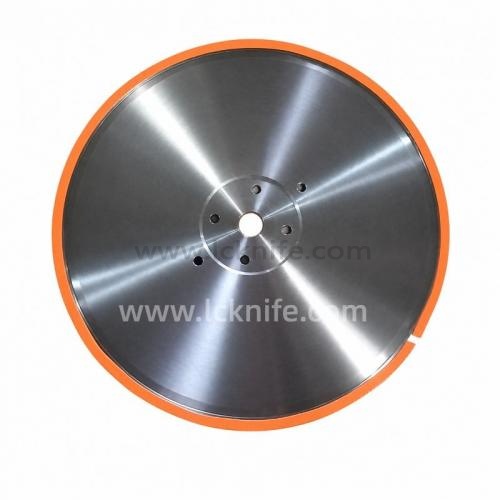
    If material selection and heat treatment represent the art of blade manufacturing, grinding is the microscopic art that ultimately determines blade life. Blade grinding involves far more than simply shaping a blade. The blade material establishes only its theoretical maximum service life; its actual surface topography is created by countless microscopic cutting traces left by the abrasive grains in the grinding wheel. At the micron—and even submicron—scale, grinding forms the cutting edge, influences surface stresses, and either creates or eliminates microscopic defects. These factors directly affect cutting accuracy, durability, and service life. Grinding is therefore an invisible yet highly precise form of microscopic craftsmanship. The quality of a ground cutting edge directly influences cutting burrs, cut-edge flatness, and blade life. Consequently, the abrasive material, grit size, grade, and structure of a grinding wheel can profoundly affect blade flatness, surface finish, and even the metallurgical microstructure of the surface layer. To significantly improve knife surface quality, the grinding process must be carefully controlled to: · Eliminate microcracks along the knife cutting edge. · Produce the optimum edge radius. · Control residual stresses in the surface layer · Control knife surface texture and roughness · Prevent grinding burns and thermally affected layers on knives. Here is a selection of grinding-wheel types Typical Application Rough-semi-finish-finish for knives Original criterion of Industry Department #25-#60 #60-#100 #100-#240 #240-W20 Reachable surface coarseness Ra0.8 Ra0.8-Ra0.4 Ra0.4-Ra0.2 Ra0.2-Ra0.05 1. Brown Fused Alumina (A): Rough Grinding and Initial Edge Formation Grinding wheel characteristics Brown fused alumina offers moderate hardness, high toughness, and good heat resistance. Rough grinding for the raw knife materials generally uses relatively coarse grit sizes, such as 46 to 60 grit. Vitrified bonds and open structures are commonly selected to provide high porosity and efficient chip clearance. Effect on blade characteristics Brown fused alumina is suitable for rapid stock removal when a large machining allowance is required. Although it provides high grinding efficiency and makes blade flatness relatively easy to control, it produces a comparatively poor surface finish. The resulting surface has a higher Ra value and clearly visible grinding marks. Effect on operating performance Brown fused alumina is primarily used for rough grinding of ordinary carbon steel blades and low-alloy tool steel knives such as 9CrSi knives. It can quickly remove heat-treatment scale and excess material. However, if it is used directly for finishing grinding, the rough cutting edge can increase friction during shearing, causing burrs on the processed material. 2. White Fused Alumina (WA): Efficient Finish Grinding of Hardened-Steel Blades Grinding-wheel characteristics White fused alumina is harder than brown fused alumina....
    View More
  • Maanshan Licheng blade manufacturing co., LTD. wishes you a happy Mid-Autumn Festival
    Sep 21, 2026 Maanshan Licheng blade manufacturing co., LTD. wishes you a happy Mid-Autumn Festival
    As the bright full moon rises on the 15th day of the eighth lunar month, we welcome the Mid-Autumn Festival—a cherished traditional Chinese celebration. Bathed in the warm glow of togetherness, communities across the country come alive with peace and festive cheer. From gazing at the luminous moon and savoring sweet mooncakes to strolling through lantern fairs and experiencing rich intangible cultural heritage, people gather to celebrate family reunions and feast on a profound cultural tradition. For centuries, the mid-autumn moon has mirrored the deepest emotional ties of the Chinese people. No matter how far away they travel, their longing for home and blessings for loved ones flow gently beneath the moonlight. Today, we also extend heartfelt holiday gratitude to the builders, medical personnel, and volunteers standing firm at their posts; a simple mooncake and a warm greeting bring the comforting embrace of a large family. In neighborhoods and schools, "Celebrating Mid-Autumn Together" events invite international students and overseas friends to taste mooncakes and listen to the mythological tale of Chang'e flying to the moon—allowing the world to share in this uniquely Chinese romance. Maanshan Licheng Blade Manufacturing Co., Ltd. delivers superior cutting performance from the inside out. By utilizing top-tier global and local materials alongside advanced processing techniques—such as vacuum, sub-zero, and salt-bath heat treatments—we engineer blades with exceptional structural integrity and durability.Should you have any questions or needs regarding for metallurgy industrial blades , paper industrial knife , or other applications, please feel free to reach out to us at any time.
    View More
  • Optimization of Heavy Plate Shearing Blades: Performance Advantages and Application Guidelines for H13 Tool Steel
    Sep 08, 2026 Optimization of Heavy Plate Shearing Blades: Performance Advantages and Application Guidelines for H13 Tool Steel
    When processing medium and heavy plates, the thickness generally ranges from 8 to 60 mm, with hot rolling as the main method of manufacture. The materials usually employed are Q235, Q345, various high-strength steels, and similar ones. To reduce cutting-induced defects in the cross-section, shearing is performed at high temperatures, typically between 400°C and 700°C. Four Core Challenges in Heavy-Duty Shearing of Knives 1. High Temperature: When the temperature is high, the martensite in the tool undergoes tempering and breaks down into ferrite and large carbides, causing the matrix to become softer. At 400°C, cementite (Fe3C) begins to coarsen and lose effectiveness; as a result, the blade loses hardness and fails. 2. Oxide Scale: The presence of iron oxide scale on the surface of hot-rolled plates results in increased abrasive wear of the tool. The knife's cutting edge gradually rounds off, thereby losing its sharpness, which in turn unintentionally increases the tool clearance and leads to larger shearing burrs on the steel plate. 3. Fatigue: The hardness of the oxide scale on the surface of the plate is considerably greater than that of the base metal; it is brittle and abrasive and thus acts as the main reason for shearing tool wear and failure. At the same time, thermal-cycling shearing conditions increase fatigue effects. 4. Impact Load: When it comes to impact load, the thickness of hot-rolled plates is usually not uniform, and the brittle oxide scale breaks apart on impact, resulting in local stress peaks at shearing edges; under repeated impacts, the microscopic cutter edge defects grow so that small pieces of the surface material flake off from the knife and knife edge chipping occurs. Shearing Targets for Heavy Plates. Within the above demanding operational conditions, steel mills encounter considerable challenges in achieving the specified shearing criteria: 1.Shearing burr within < 3%–5% of plate thickness. 2.The length tolerance of the plate sheet after cutting is within plus or minus 0.5 to 1 mm, and the cut must be perpendicular. 3.Clean cross-section free from tearing, nodulation, or edge collapse. 4.Blade lifespan capable of supporting batch production with low tool-change frequency. Alloy Composition and Performance of H13 Tool Steel To address the challenging problems associated with heavy plate shearing, LCKNIFE chose H13 (1.2344, 4Cr5MoSiV1) tool steel for its advantageous composition. 1.Carbon (C: 0.32–0.45%): Contributes to the matrix quenching hardness and basic wear resistance; the medium carbon content ensures toughness of the knife without causing brittleness. 2.Silicon (Si: 0.80–1.25%): Improves the hardenability of knife steel and enhances oxidation resistance and thermal fatigue resistance. · 3.Manganese (Mn: 0.20 to 0.60%): Helps the tool’s hardenability. 4.Chromium (Cr: 4.75–5.50%): Gives excellent hardenability, forms chromium carbides, and has good resistance to oxidation at high temperatures in a knife. 5....
    View More
  • Golden Autumn September Sets Sail on a New Journey: Schools Across the Country Welcome the First Day of Class
    Aug 31, 2026 Golden Autumn September Sets Sail on a New Journey: Schools Across the Country Welcome the First Day of Class
    Heartwarming Reunions: The middle and high school campuses presented a lively scene of old friends reuniting. Many classes helped students quickly transition from "vacation mode" to "study state" by sharing vacation experiences and exchanging blessing cards. A Unique "First Class": Fostering Patriotism to Build a Solid Foundation for Growth As the grand finale of the opening day, distinctive "First Classes of the Semester" were staged brilliantly across the country. This year's classes closely followed the pulse of the times, organically combining patriotic education, the inheritance of traditional culture, and psychological counseling. Many schools invited role models, frontline scientific researchers, or outstanding youth representatives into the classroom, using vivid stories to guide teenagers in establishing lofty ideals. Through entertaining and educational methods, children received a profound spiritual baptism on their first day of school, cultivating a sense of patriotism and gathering strength for the new semester. Technology Hand in Hand with Reducing Burdens: Opening a New Experience in Smart Education Notably, the new semester's campuses also shined with the highlights of "technological empowerment" and the quality enhancement of the "double reduction" policy (reducing excessive homework and off-campus tutoring). Many schools introduced a virtual-fusion smart learning environment, comprehensively helping students develop morally, intellectually, physically, aesthetically, and labor-wise through personalized teaching and rich after-school extension courses. A new semester, a new starting point, a new hope. Accompanied by the bell of golden autumn, countless students are greeting the morning light, setting sail with full vigor, running bravely on the track of youth, and writing their own brand-new chapters. Licheng blade manufacturing, together with all our staff, extends our most sincere greetings to teachers, students, and parents across the country: We wish everyone a happy new semester, success in pursuing your dreams, and brilliant new achievements!
    View More
  • Application Breakthrough and Process Analysis of LD (7Cr7Mo2V2Si) Steel in Shear Blades for 6–8mm Q345 (Q355) Steel Plates
    Aug 28, 2026 Application Breakthrough and Process Analysis of LD (7Cr7Mo2V2Si) Steel in Shear Blades for 6–8mm Q345 (Q355) Steel Plates
    In metal processing and manufacturing, the service life and stability of shear blades are critical determinants of production efficiency and operating costs. Addressing the demanding requirements of shearing 6–8mm thick Q345 steel plates, Licheng Blade has developed high-performance shear blades using the novel cold-work die steel LD, following extensive research into end use and material innovation. End users demonstrate that these blades achieve a fourfold increase in service life compared to traditional cold-work die steels such as SKD11, hot-work die steels like H13, and W6Mo5Cr4V2 high-speed steel, thereby resolving longstanding challenges related to blade chipping, limited service life, and difficulties in regrinding. 1. Main Problems of Shear Blades Made of Traditional Materials Traditional shearing blades have been tested with various die steels and high-speed steels, but practical production continues to reveal issues that negatively affect efficiency, precision, and cost. Edge Design and Usage Limitations: I.Wedge Angle vs. Strength: When it comes to knife cutting, like a pair of scissors, a smaller angle cuts more sharply but reduces strength and shortens life, while an excessive angle increases resistance. Blade angles generally range from 80° to 90°, with 90° typically chosen to maximize the number of available cutting edges. II.Overlap Angle Range: The included angle between dual edges during transverse shearing is 0–10 degrees, while longitudinal slitter blades intersect orthogonally. III.Bite Depth and Clearance: Edge engagement requires a balance of tightness and depth. Clearance and depth affect the sheared cross-section and blade life and must be analyzed based on the shearing method, tool dimensions, and sheet thickness. IV.Shear Root Design: Improper shear root height compromises the knife cutting edge. Thicker sheets generally need larger knives, and design thickness should be at least three times the material thickness. If the knife's outer diameter or width is larger than expected, this proportion can be reduced accordingly. Manufacturing and Process Challenges: Material selection, forging, heat treatment, and grinding. These complex processes rely heavily on extensive production experience. Operational Issues: I.Blunting and Wear: Low fatigue strength leads to edge wear and localized chipping, requiring frequent replacement or removal of large fatigue layers, which severely reduces productivity. II.Brittle Fracture Failure: This is the most severe failure mode on the knife working. While fatigue failure indicates poor wear resistance, brittle fracture can cause catastrophic interruptions in steel sheeting production or safety incidents and is closely tied to material selection. 2.Breakthrough Solution: The Advantages of LD Die Steel When shearing thick plates such as 6–8mm Q345 low-alloy high-strength structural steel, slitting blades must withstand extreme impact loads and frictional shear forces. The previous material c...
    View More
  • Advanced Metallurgy, Superior Precision: Inside Maanshan Licheng Blade Manufacturing Co., Ltd.
    Aug 18, 2026 Advanced Metallurgy, Superior Precision: Inside Maanshan Licheng Blade Manufacturing Co., Ltd.
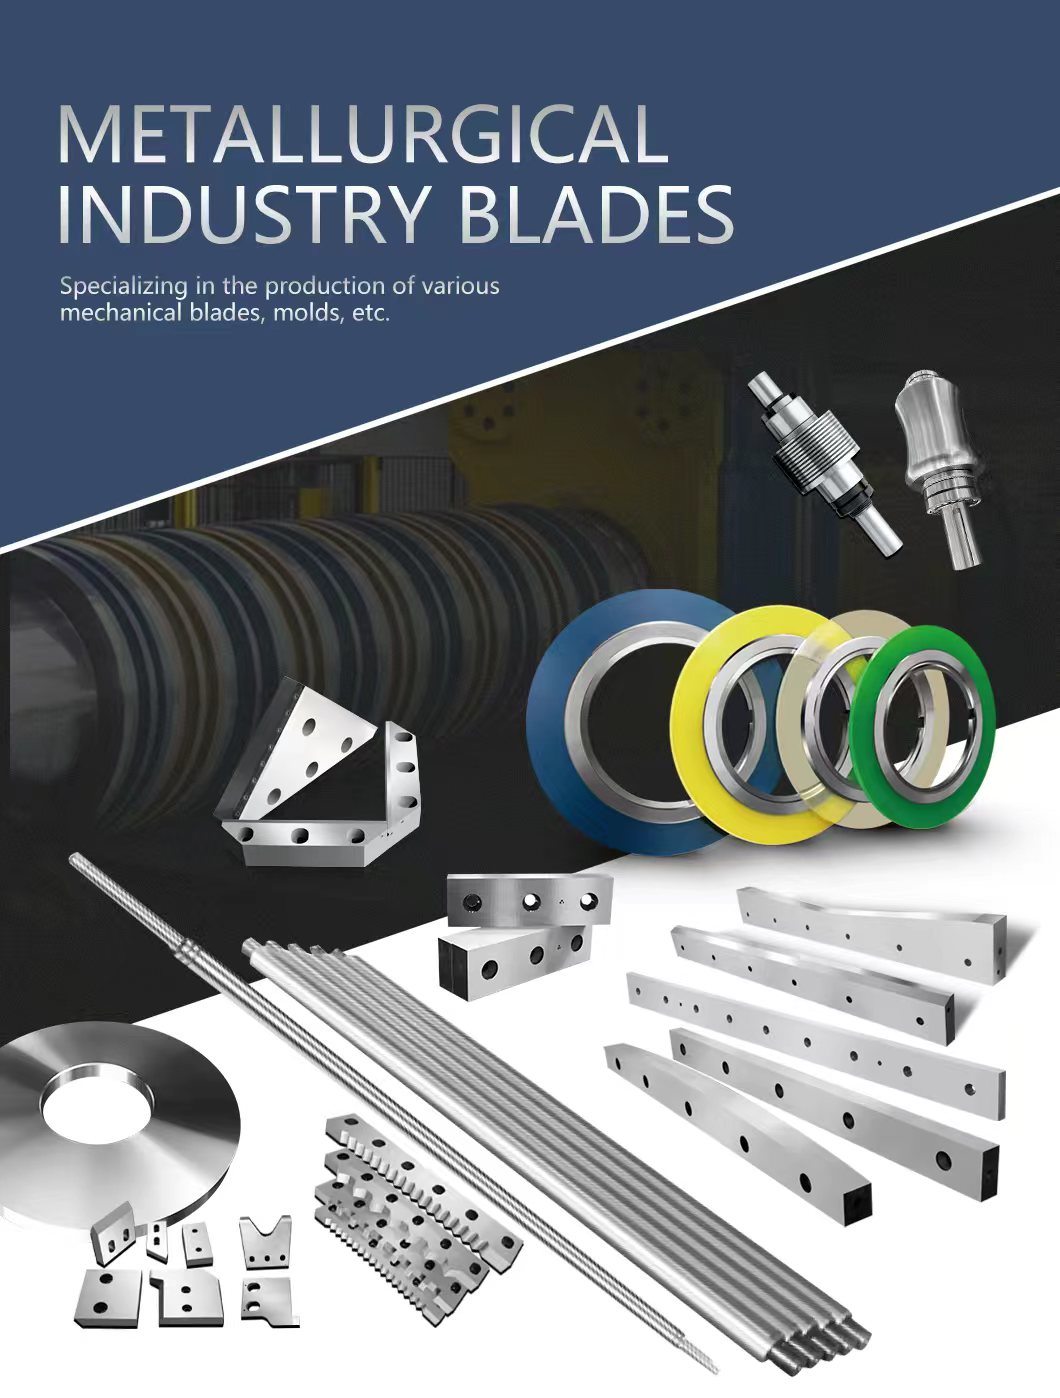
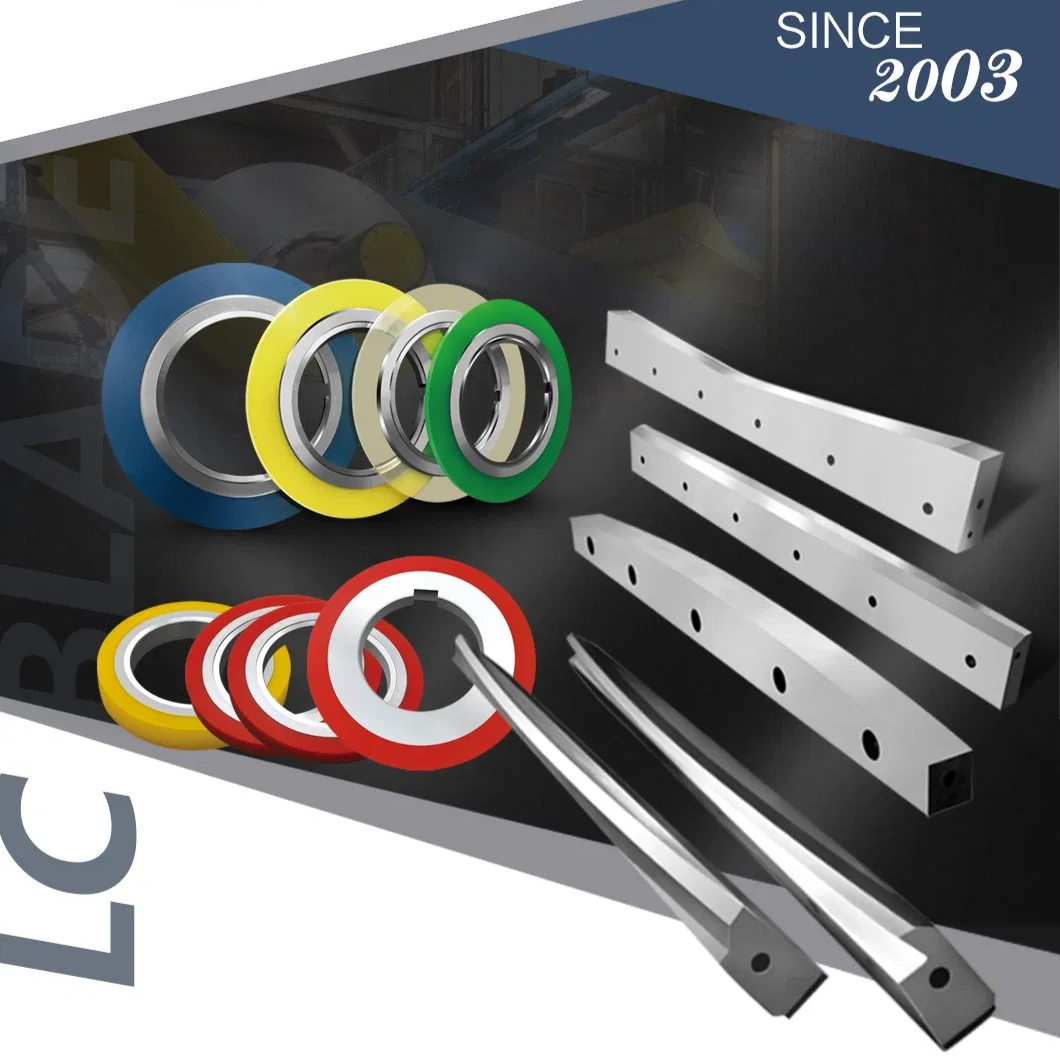
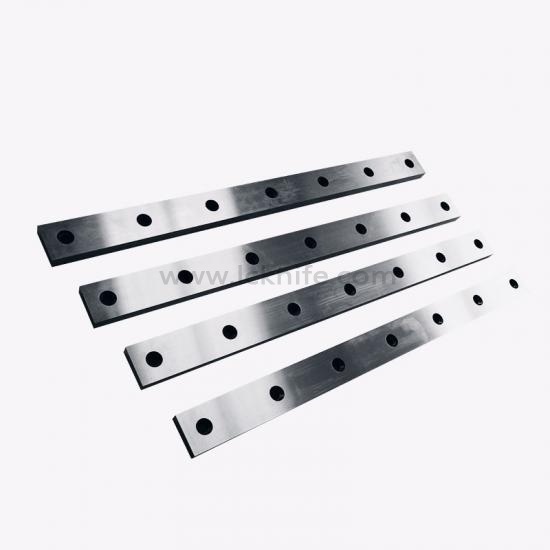
    MAANSHAN, CHINA — In the demanding world of modern manufacturing and metal processing, the quality of a cut begins long before the machine is turned on—it starts in the metallurgy and heat treatment of the blade itself. Maanshan Licheng Blade Manufacturing Co., Ltd. has established itself as a trusted leader in this space, combining elite material science with cutting-edge production techniques to deliver industrial cutting tools built for ultimate durability and precision.   At the core of Licheng’s manufacturing philosophy is an uncompromising dedication to material integrity. The company utilizes a comprehensive selection of both high-quality imported and premium domestic materials, carefully chosen to match the rigorous demands of heavy industry. However, selecting the right raw steel is only the first step. To unlock the full potential of the metal, Licheng employs a suite of advanced heat treatment processes, including:   Vacuum Heat Treatment: Minimizes distortion and surface oxidation, ensuring structural uniformity throughout the blade.   Subzero Heat Treatment: Drives retained austenite out of the steel, significantly boosting wear resistance and dimensional stability.   Salty Bath Heat Treatment: Provides rapid, uniform heating for exceptional hardness and toughness balance.   These sophisticated thermal processes fundamentally enhance the inner character and micro-structure of every knife, resulting in superior edge retention, impact resistance, and an extended operational lifespan even under extreme industrial conditions.     Specialized Solutions for the Metallurgical Industry While Licheng caters to a diverse global industrial base, the company is primarily renowned for its specialized engineering of metallurgical industry blades. Designed to withstand high-stress environments, heavy thermal loads, and continuous operation, Licheng’s core product lineup includes:   Round coil slitting knives - Manufactured to exact tolerances for smooth, burr-free rotary cutting and slitting applications across various metal gauges. Suitable for mild, chopper, aluminum steel, pickling lines, silicon steel etc. Cutting capacity ranging from 0.05mm to 25mm thick coil strips.   Steel shear blade - The surface finish has a great impact on the accuracy and durability of the steel shear blade. The grinding surface of the blade is actually formed by countless scratches scored by a large number of abrasive particles on the grinding wheel. Engineered for clean, high-precision shearing of heavy plates, offering exceptional impact toughness to prevent chipping or cracking under high tonnage.   Silicon Steel Slitting Blades: Specially crafted for the high-precision processing of electrical silicon steel—a material notorious for demanding flawless edge quality and extreme wear resistance to prevent burrs that could compromise electrical core performance.   Through the synergy of classic craftsmanship and in...
    View More
  • New Safety Standards Issued for Automated Meat Slicer Blade Guards
    Aug 05, 2026 New Safety Standards Issued for Automated Meat Slicer Blade Guards
    The Food Safety and Inspection Service, in collaboration with commercial kitchen safety boards, has officially issued updated safety standards regulating automated meat slicer blade guards. The new directive aims to drastically reduce workplace injuries and cross-contamination risks in commercial delis, supermarkets, and food processing facilities. Under the updated 2026 regulations, all newly manufactured automated meat slicers must feature enhanced, heavy-duty blade guards that prevent accidental operator contact during both operation and high-speed cleaning cycles. Statistics show that meat slicer blades remain one of the leading causes of severe lacerations in the foodservice industry, often occurring when guards are removed for sanitation. Industry Impact and Future Outlook: Moving Toward a Zero-Injury Modern Transformation The official rollout of the 2026 slicer safety standards marks the food retail and processing industry’s goodbye to the era of rough management that traded safety for cleaning efficiency. For equipment manufacturers, this directive is an urgent technical challenge, pushing them to invest more in ergonomics, quick-clean structures (allowing easy maintenance without compromising safety), and smart interlock systems. For business managers and employers, while there are initial costs for updating equipment, in the long run, it will significantly reduce legal disputes from workplace injuries, insurance claims, employee turnover, and recall crises caused by food contamination.
    View More
  • How to Prevent Distortion and Cracking in Ultra-Long Shear Blades
    Jul 20, 2026 How to Prevent Distortion and Cracking in Ultra-Long Shear Blades
    In modern metal fabrication, ultra-long CNC shear blades (exceeding 3 meters) demand absolute precision. Achieving flawless parallelism, straightness, and uniform hardness is a major challenge. Because these components are exceptionally long, they are highly prone to thermal distortion and cracking during the heat treatment process. How can manufacturers prevent these critical defects? The secret lies in precise material selection and a strict, two-stage preheating protocol. 1. Choose the Right High-Alloy Tool Steel Preventing failure starts with metallurgy. For heavy-duty, extra-long shear blades, standard steels won’t suffice. Industry leaders rely on premium high-alloy tool steels like Cr12MoV, DC53, LD, and H13K. These materials offer the high wear resistance and core toughness required to withstand immense shearing forces without snapping or warping. 2. Implement a Two-Stage Preheating Process During the heating cycle, steel naturally expands. However, upon reaching its phase transition point, the material undergoes volumetric contraction. In a 3-meter integrated blade, this uneven expansion and contraction creates massive internal stresses, leading to warping or cracking. To eliminate this stress, a two-stage preheating technique is essential before final quenching: Stage 1 (Isothermal Soaking): Heat the blade to 500°C and hold it at an isothermal state. This ensures uniform temperature from the core to the surface. Stage 2 (Transition Heating): Gradually ramp the temperature up to 850°C for a second preheat before raising it to the final quenching temperature. Minimizing heat treatment distortion in ultra-long shear blades requires strict tolerance control. By utilizing advanced alloys like DC53 or H13K and mastering the two-stage preheating cycle, you can drastically reduce internal stress, eliminate cracking, and ensure perfect blade straightness for high-precision CNC cutting operations.
    View More
first page 1 2 3 ... 13 last page

A total of 13 pages

Newsletter

Please read on, stay posted, subscribe, and we welcome you to tell us what you think.

Leave a message
welcome to Licheng
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.

Home

Products

about

contact